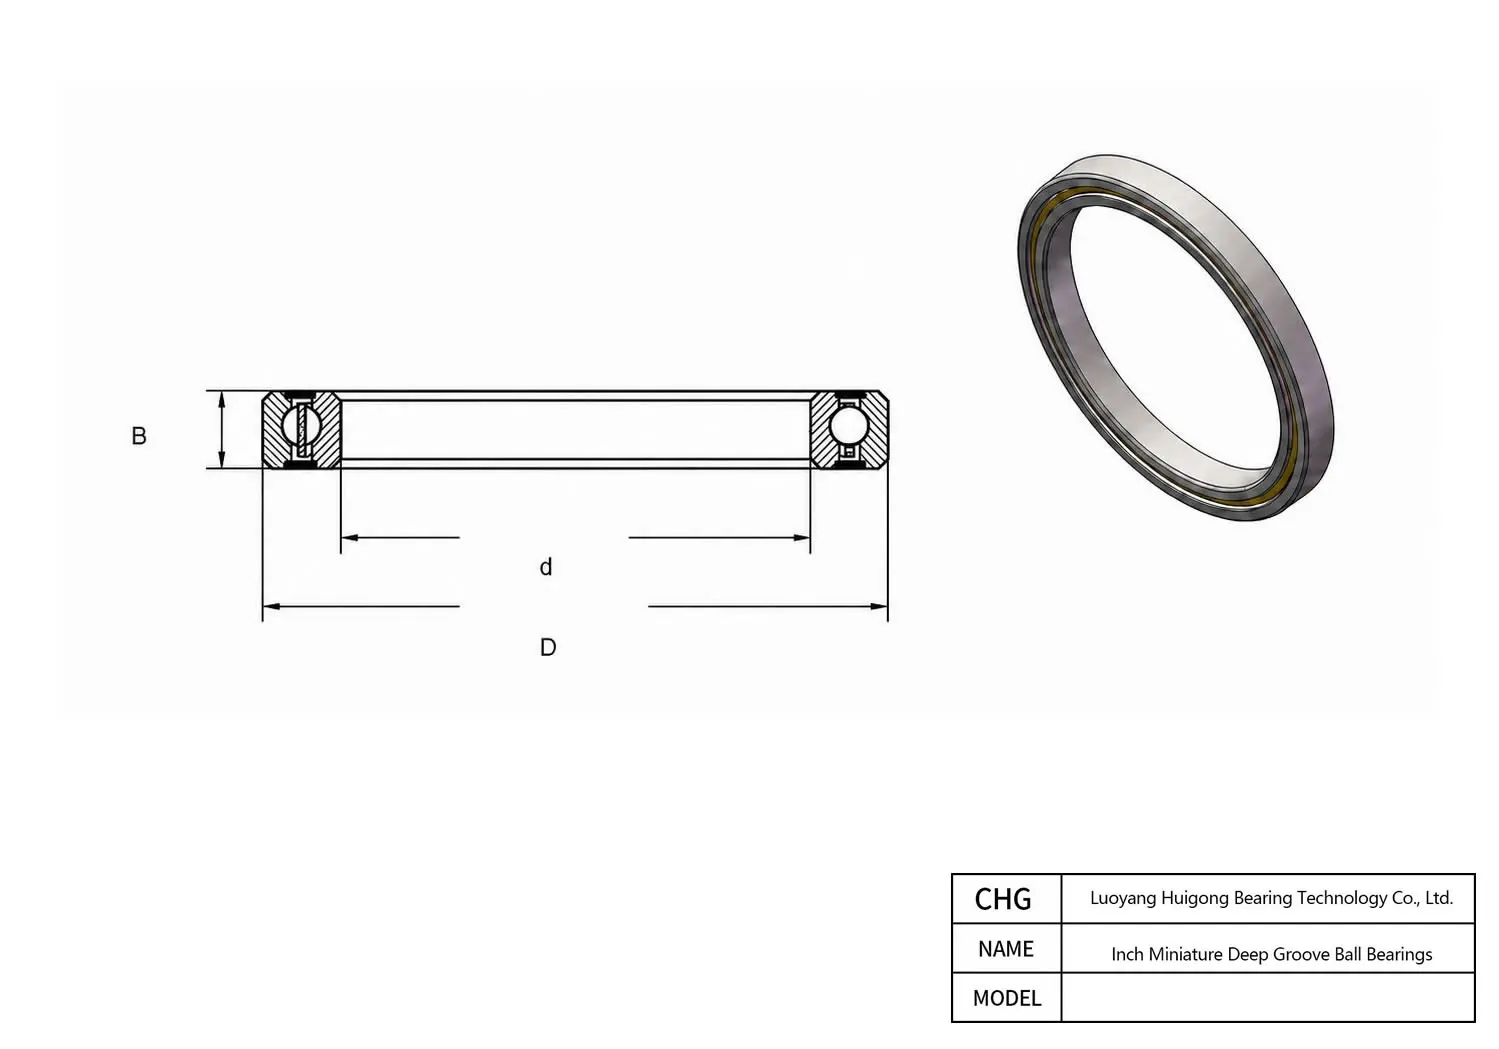
Manufactured by CHG Bearing, the R155* is a precision Inch Miniature Deep Groove Ball Bearings. Key dimensional parameters include a 3.967 mm bore diameter, a 7.938 mm outer diameter, and a 2.779 mm overall width. This component is designed to meet standard load requirements and ensure consistent operational performance. For comprehensive technical evaluation, please explore the detailed specifications, dimensional data, product images, and CAD drawings provided below. A complete PDF data sheet is also readily available for direct download to support your engineering and procurement needs.
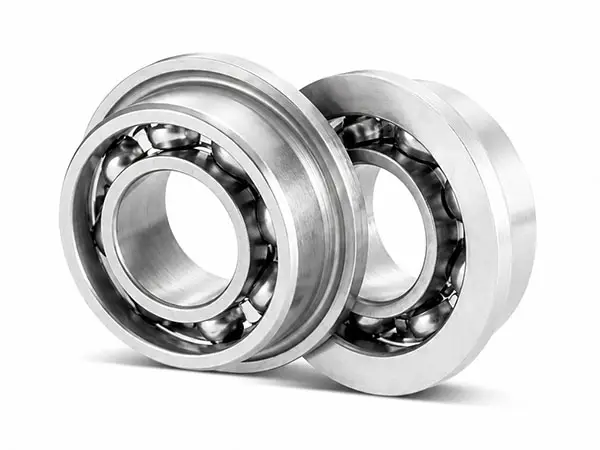
R155* - Inch Miniature Deep Groove Ball Bearings
Technical Specifications
| Overview | |
|---|---|
| Part Number | R155* |
| Dimensions | |
| Bore Diameter (d) | 3.967 mm |
| Width (B) | 2.779 mm |
| Outer Diameter (D) | 7.938 mm |
| Open Width B | 2.779 mm |
| Radius rs min | 0.1 mm |
| Flange Df | 9.119 mm |
| Closed Width B1 | 3.175 mm |
| Open Flange Width Bf | 0.584 mm |
| Closed Flange Width Bf1 | 0.914 mm |
| Performance | |
| Dynamic Load Cr (N) | 359 N |
| Static Load C0r (N) | 150 N |
| Grease Speed (x1000 rpm) | 53 x1000 rpm |
| Oil Speed (x1000 rpm) | 63 x1000 rpm |
| Design Configurations | |
| Open Model | R155* |
| Flanged Open Model | FR155* |
| Shielded Model | R155ZZS* |
| Flanged Shielded Model | FR155ZZS* |
| 2RS | - |
| 2RU | - |
| TTS | - |
| Internal Design & Weight | |
| Cage Type | W |
| Ball Qty. Z | 10 |
| Ball Size Dw | 1 mm |
| Shielded Weight (g) | 0.61 g |
| Flanged Shielded Weight (g) | 0.72 g |
| Open Weight (g) | 0.51 g |
| Flanged Open Weight (g) | 0.58 g |
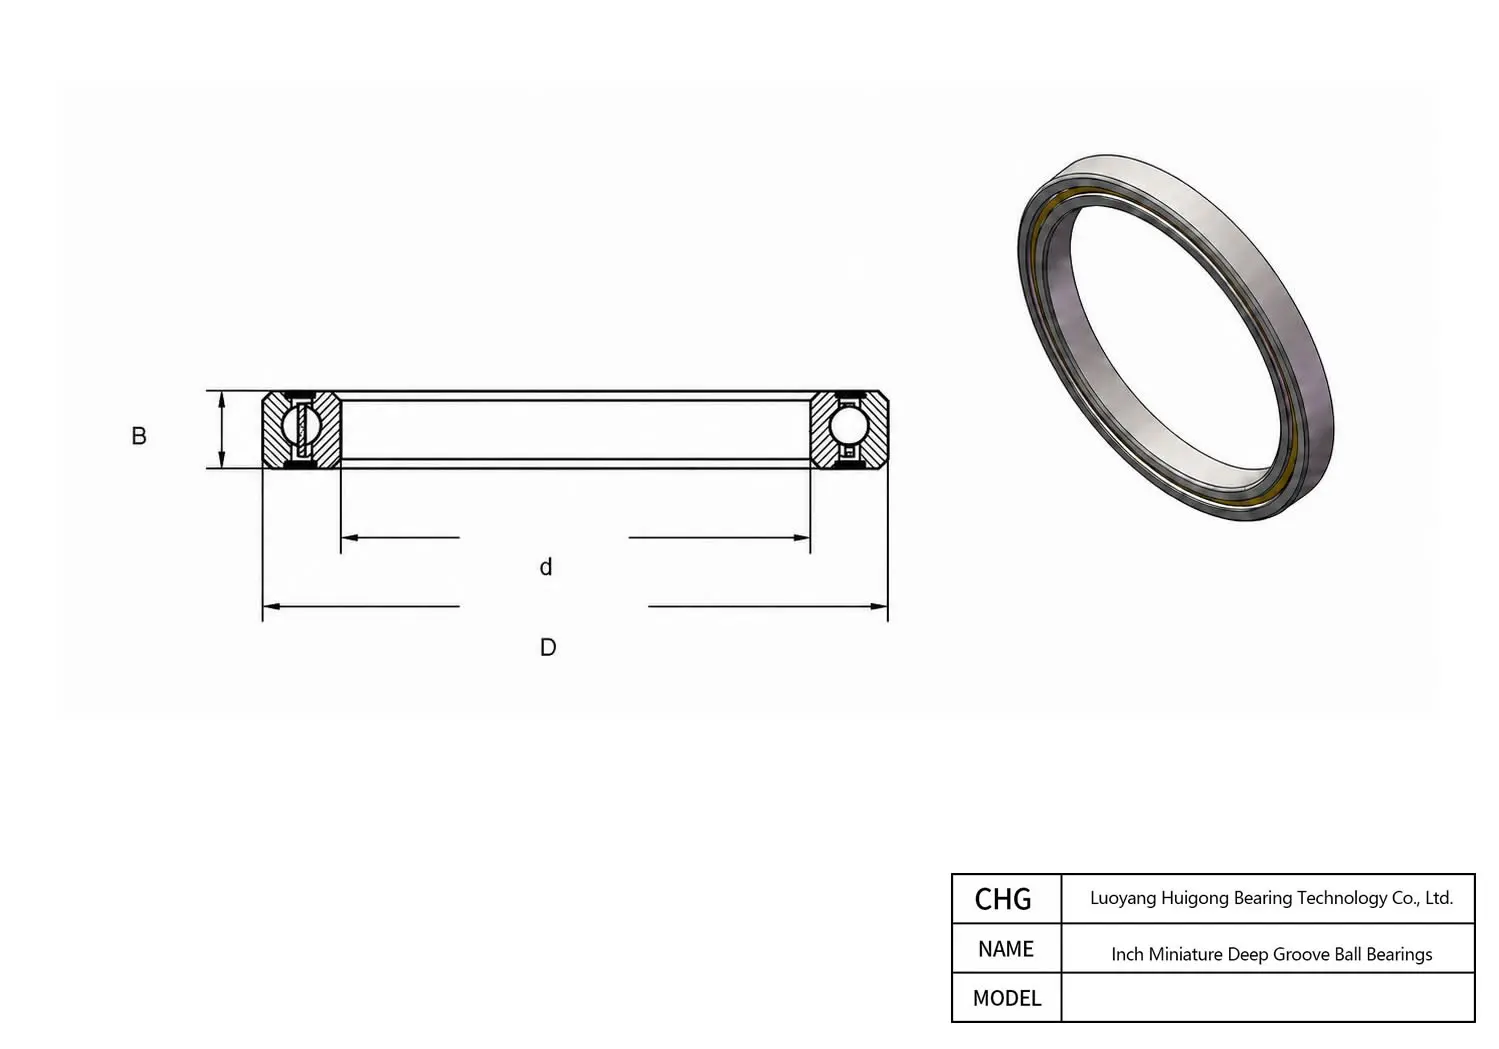 R155* 7.938 mm 3.967 mm 2.779 mm
Frequently Asked Questions about R155* Inch Miniature Deep Groove Ball Bearings
Find key technical answers regarding dimensions, specifications, and replacement options for this model.
In its sealed configuration (Open Type), CHG Bearing pre-charges R155* with premium wide-temperature lithium-complex or polyurea grease, calibrated to a 30%–35% cavity volume ratio. For open-type variants, synthetic PAO or refined mineral lubricating oils with appropriate EP (Extreme Pressure) additives should be circulated.
When fitting R155* over a 3.967 mm shaft, CHG Bearing strictly recommends uniform induction heating (controlled between 90°C and 110°C) or precision hydraulic press sleeves. Under no circumstances should direct impact blows be struck against the rings or cage, as shock loads cause brinelling indents and premature spalling.
As standard production, CHG Bearing subjects R155* to precision bainite or martensite quenching, offering dimensional stability up to 120°C (248°F). For high-heat processing equipment, CHG Bearing also supplies custom S0 (150°C), S1 (200°C), or S2 (250°C) stabilization heat treatments upon request to prevent residual austenite transformation.
To safeguard CHG Bearing R155* against fretting wear and false brinelling during transport or vibration, assemble mating surfaces (3.967 mm x 7.938 mm) using anti-fretting mounting paste. Maintaining strict alignment and avoiding prolonged static vibration will preserve raceway polish.